How to assess PPAP readiness of automotive sensor system manufacturers




A sensor supplier can deliver convincing prototypes and still be unprepared for production approval. The gap often appears when buyers request evidence from the intended manufacturing line: measurement studies are incomplete, validation samples cannot be linked to production records, or calibration settings differ from the released specification. These gaps can delay approval and leave sourcing teams committed before manufacturing risks are understood.
To assess PPAP readiness of automotive sensor systems manufacturers, verify three things first: the applicable customer requirements are defined, the evidence represents the proposed production configuration, and unresolved risks have a credible closure plan. A completed document checklist is not enough. The strongest assessment follows a critical sensor characteristic from its design requirement through manufacturing controls, measurement results, validation, and submission status.
Define the approval boundary before requesting documents
Production Part Approval Process, or PPAP, establishes whether a supplier understands the engineering requirements and whether its production process can consistently meet them under the required conditions. Readiness means the supplier can support the required submission with valid evidence; it does not mean the customer has approved the part.
Start by agreeing exactly what is being approved. A sensing element, packaged sensor, and integrated sensor module have different evidence needs. For an electronic assembly, the boundary may include embedded firmware, calibration data, connectors, housing, and interfaces—not just the physical part number.
- Part identity: Customer and supplier part numbers, drawing revisions, specification revisions, and applicable software or calibration versions.
- Manufacturing scope: Production site, line, tooling, cavities, test equipment, and outsourced operations.
- Submission rules: Applicable PPAP framework, submission level, customer-specific requirements, and required approval authority.
- Program timing: Production trial, validation completion, submission date, customer review, and planned shipment authorization.
Do not interpret a lower submission level as permission to omit underlying work. Submission levels generally determine which evidence is submitted or retained, subject to customer requirements. Ask the supplier to map each applicable requirement to an owner, evidence location, status, and due date. Items marked “not applicable” should have a documented rationale and customer agreement where required.
Follow one critical characteristic through the evidence
A pressure sensor may meet room-temperature accuracy requirements but drift outside limits after environmental exposure. A position sensor may pass electrical testing while assembly variation changes its output relationship. Such risks are easier to assess by tracing a characteristic end to end than by reviewing separate files in isolation.
Select a characteristic with engineering input: output accuracy, response time, leak tightness, insulation resistance, or another requirement significant to the application. Then compare the evidence below.
Where the supplier has design responsibility, review the applicable design FMEA as well. For build-to-print supply, confirm how the supplier receives critical requirements and communicates manufacturing concerns. Lack of design ownership does not remove responsibility for controlling production risks.
Challenge measurement capability before accepting capability indices
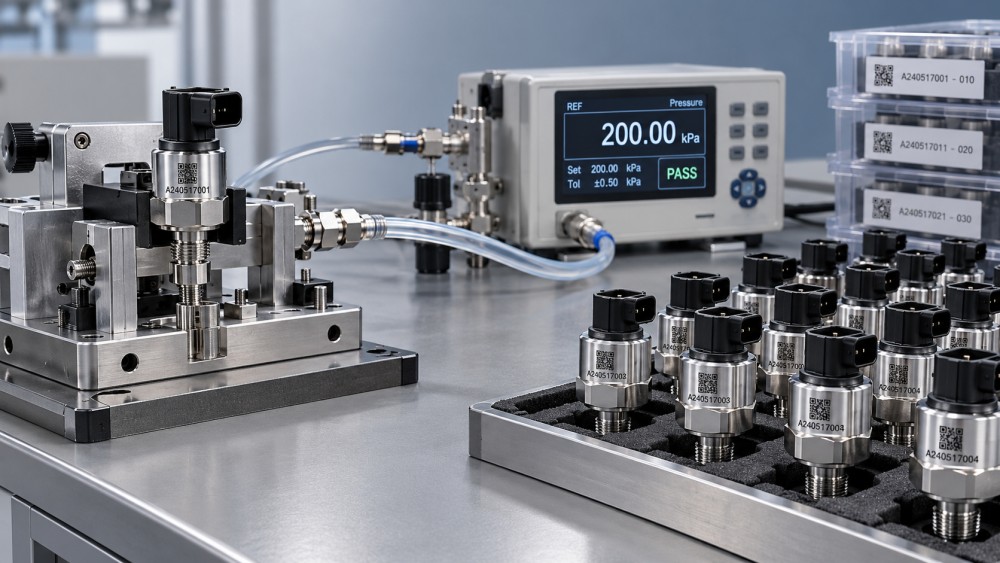
Sensor acceptance often depends on a complete measurement chain: reference stimulus, fixture, power supply, acquisition hardware, software, and compensation settings. A calibrated reference instrument alone does not establish that this chain is suitable for the acceptance decision.
Request measurement system analysis appropriate to the method. Variable measurements may require assessment of repeatability, reproducibility, bias, linearity, and stability as applicable. Attribute decisions, such as an automated pass/fail classification, need evidence that the system reliably distinguishes acceptable and unacceptable parts, especially near decision limits.
Ask how the supplier handles temperature stabilization, fixture variation, reference uncertainty, and operator influence. For automated stations, examine station-to-station correlation and controls over test software. Where testing is destructive or parts cannot be measured repeatedly without changing them, the study design needs a justified alternative rather than a conventional study applied mechanically.
Only then review process capability. Confirm that the data represents the required production conditions, measurement systems, and sampling method. Check process stability and distribution assumptions before relying on Cpk or Ppk. Acceptance thresholds must follow customer requirements; a familiar industry target should not be substituted for the program’s actual criteria.
Calibration deserves particular attention. Determine whether capability results represent performance before or after adjustment, how adjustment limits are controlled, and whether excessive correction signals an upstream problem. A passing final result can conceal a process that relies on repeated tuning or selective retesting.
Separate production evidence from prototype success
Ask which records came from the intended production tooling, equipment, materials, operators, and process sequence. Samples assembled with laboratory methods may support development but do not automatically demonstrate production readiness.
Review the planned or completed significant production run against the applicable customer requirements. The supplier should identify quantities, operating conditions, shifts where relevant, interruptions, scrap, rework, and equipment changes. Do not impose a universal run duration or quantity without checking the governing requirements.
Look beyond the submitted good parts
Yield and retest history show whether the submitted results reflect routine production. Request the disposition of failed units and the rules for retesting. An unexplained practice of repeating a test until a unit passes undermines confidence in acceptance data.
Capacity is a related but separate decision. A PPAP package does not, by itself, demonstrate that the supplier can sustain contracted volume. Examine cycle time at calibration and end-of-line stations, maintenance coverage, changeovers, and any customer-required capacity verification. Keep capacity gaps visible even when the documentation is otherwise ready.
Match validation to the sensor’s actual application
A report labelled “automotive qualified” is not sufficient evidence for a specific sourcing decision. Compare validation coverage with the released requirements and intended mounting location, electrical environment, media exposure, and operating conditions.
Depending on the sensor and specification, relevant evidence may include thermal cycling, vibration, humidity, electrical disturbances, electromagnetic compatibility, ingress protection, media compatibility, and performance after exposure. These are examples, not a universal test program. The applicable specification determines the conditions, sample sizes, sequences, and acceptance criteria.
For each required test, establish:
- Whether the sample construction, firmware, calibration, and manufacturing process match the proposed production configuration.
- Whether the method and acceptance limits match the approved requirement revision.
- Whether deviations, failures, and corrective actions are documented and resolved or formally accepted.
- Whether subsequent changes require additional testing or a justified engineering assessment.
Review individual results and failure dispositions, not only a green summary page. Testing on an earlier sealing material or circuit revision may not cover the current product. Where functional safety or cybersecurity requirements apply, involve the responsible specialists to assess the relevant evidence; PPAP does not replace those engineering assessments.
Test traceability with a sample record retrieval
Ask the supplier to retrieve the manufacturing history for a selected finished sensor. The exercise should establish whether records are connected and usable, rather than whether the supplier owns traceability software.
Depending on agreed requirements, the history may need to identify component lots, sensing-element source, assembly conditions, calibration coefficients, firmware version, test results, rework status, and shipment information. Serialization is not automatically required for every application, but the traceability granularity must support the customer’s containment expectations.
Then reverse the exercise: choose a suspect incoming component lot or test-station fault and ask which finished products would be contained. The supplier should explain how it defines the affected population and prevents release while the issue is investigated.
Include sub-tier controls. Purchased sensing elements, electronic components, seals, and outsourced processing can affect performance even when final assembly remains unchanged. Review supplier qualification, incoming controls, change notification, and how sub-tier evidence supports the final submission. A distributor certificate alone may not establish the manufacturing traceability required by the customer.
Turn open gaps into a sourcing decision
Use a readiness review with procurement, supplier quality, and engineering rather than allowing document completeness to determine the outcome. Distinguish evidence that is complete, evidence awaiting verification, open technical work, and items awaiting customer disposition. A scheduled test is not completed evidence.
Conditional progression is an internal sourcing decision, not permission to ship unapproved production parts. Any interim approval, deviation, or shipment authorization must come through the applicable customer process and specify its limits.
For each open item, record the affected requirement, risk, containment, owner, closure evidence, deadline, and decision authority. Tie commercial milestones to meaningful evidence where appropriate, rather than a promise that “PPAP will follow.”
Finally, examine change control before closing the assessment. Ask how the supplier evaluates a sensing-element substitution, firmware update, fixture change, production transfer, or calibration algorithm revision. The process should identify when customer notification, additional validation, or PPAP resubmission is required. A supplier whose approval evidence cannot remain connected to the configuration it ships is not ready for a dependable production release.
Related News
- 00
0000-00
How to assess PPAP readiness of automotive sensor system manufacturers - 00
0000-00
What to ask an FPC connector manufacturer about reliability testing - 00
0000-00
How to verify vehicle fitment for an aftermarket AC evaporator - 00
0000-00
How electric compressor speed affects EV battery cooling capacity - 00
0000-00
How to verify a variable frequency compressor supplier’s efficiency claims
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.
Recommended News
 How to assess PPAP readiness of automotive sensor system manufacturersAssess Automotive Sensor Systems manufacturers for PPAP readiness. Learn to verify production evidence, measurement capability, validation, and traceability to reduce sourcing risks.Author:Time:Oct 22, 2026
 What to ask an FPC connector manufacturer about reliability testingChoosing an FPC Connector manufacturer? Learn what to ask about reliability testing, failure limits, and traceable results to reduce design risks and select with confidence.Author:Time:Oct 21, 2026
 How to verify vehicle fitment for an aftermarket AC evaporatorNavigating the evaporator aftermarket? Verify vehicle fitment with VIN data, OE numbers, and physical interface checks. Use this guide to avoid costly mismatches and order confidently.Author:Time:Oct 20, 2026
 How electric compressor speed affects EV battery cooling capacityElectric compressor technology: battery cooling depends on more than RPM. Discover how speed, refrigerant flow, and system limits affect EV cooling capacity and energy efficiency.Author:Time:Oct 19, 2026
 How to verify a variable frequency compressor supplier’s efficiency claimsVerify a variable frequency compressor supplier’s efficiency claims using COP boundaries, matched test conditions, and duty-cycle data. Learn how to choose with confidence.Author:Time:Oct 18, 2026
 How bend radius affects FPC reliability in automotive camera modulesAutomotive FPC applications: camera module reliability starts with bend radius. Learn how stack-up, strain, and validation guide robust designs and help prevent costly failures.Author:Time:Oct 17, 2026
 How to diagnose intermittent loss of electric power steering assistMaster power steering system diagnostics to trace intermittent EPS assist loss. Learn proven checks for voltage, wiring, and fault codes to avoid costly guesswork.Author:Time:Oct 16, 2026
 How to size automotive power modules for electric compressorsSize automotive power modules for electric compressors with confidence. Learn how voltage, phase current, losses, and cooling shape reliable selection—and avoid costly oversizing.Author:Time:Oct 15, 2026
 Why automotive power electronics are shifting to silicon carbideAutomotive Power Electronics are shifting to silicon carbide. Discover how SiC can cut losses, boost EV power density, and reshape cooling, reliability, and system costs.Author:Time:Oct 14, 2026
 How EV adoption shapes the electrically driven compressor marketExplore how EV adoption shapes the electrically driven compressor market, from battery cooling and heat pumps to supplier margins. Discover the drivers of profitable growth.Author:Time:Oct 13, 2026
 How to size a PTC heater for reliable EV cabin heatingPTC Heater sizing for EV cabins: learn how to balance defrost performance, heat-pump integration, airflow, voltage range, and battery power for reliable winter comfort.Author:Time:Oct 12, 2026
 What determines the cooling output of electric automotive AC compressors?Automotive air conditioning compressors electric systems: explore how speed, voltage, refrigerant, controls, and heat exchangers shape EV cooling capacity and efficiency.Author:Time:Oct 11, 2026
 What makes a touchscreen media head unit responsive enough for daily use?Touchscreen media head unit performance explained: discover what delivers fast starts, smooth maps, reliable phone pairing, and responsive daily driving.Author:Time:Oct 10, 2026
 How Does a Battery Management System Communicate Cooling Demand?How does a battery management system communicate cooling demand? Explore CAN signals, thermal priorities, fault handling, and EV cooling control strategies.Author:Time:Oct 20, 2026
 Can a Domain Controller Share a Cooling Loop with Other Electronics?Can a domain controller share a cooling loop with other electronics? Explore thermal zoning, flow control, safety priorities, and reliable vehicle electronics cooling strategies.Author:Time:Oct 19, 2026
 What Causes Domain Controller Overheating During Summer Testing?What causes domain controller overheating in summer testing? Explore heat load, airflow, installation, software factors, and practical fixes.Author:Time:Oct 18, 2026
 Is a Head-Up Display Hard to Integrate with Different Windshields?Is a head-up display difficult to integrate with different windshields? Discover how glass geometry, coatings, and calibration affect HUD clarity, cost, and production readiness.Author:Time:Oct 17, 2026
 What Should Be Checked Before Selecting an Automotive Head Unit?What should be checked before selecting an automotive head unit? Explore compatibility, performance, cybersecurity, compliance, and supplier support.Author:Time:Oct 16, 2026
 Is Steer-by-Wire More Expensive Than an EPS Steering System?Is steer-by-wire more expensive than an EPS steering system? Explore the true costs, safety demands, software value, and when SbW justifies its premium.Author:Time:Oct 15, 2026
 Which Automotive Electronics Need Validation for 800V Platforms?What automotive electronics should be validated for 800V platforms? Explore critical checks for harnesses, power electronics, thermal systems, safety, and EMC.Author:Time:Oct 14, 2026
 How Do Automotive Compressor Export Requirements Vary by Market?How do automotive compressor export requirements vary by market? Explore key compliance rules for refrigerants, EV safety, OEM approvals, labeling, and customs.Author:Time:Oct 13, 2026
 What Documents Are Needed to Export Automotive Thermal Components?What documents are needed to export automotive thermal components? Explore customs, compliance, technical records, and shipping tips to prevent costly delays.Author:Time:Oct 12, 2026
 How Often Should an EV Air Conditioning Compressor Be Inspected?How often should an EV air conditioning compressor be inspected? Discover recommended service intervals, warning signs, and expert care tips to protect cooling performance and EV reliability.Author:Time:Oct 11, 2026
 How resolution and refresh rate affect vehicle dashboard displaysCompare resolutions and refresh rates of vehicle dashboard displays to optimize readability, motion, latency, and cockpit performance. Explore the right specs for every vehicle display.Author:Time:Oct 20, 2026
 How to size power solutions for automotive head-up display systemsHeads-up display systems power solutions: learn how to size automotive HUD power architectures for startup, brightness, thermal limits, EMC, protection, and reliable vehicle operation.Author:Time:Oct 19, 2026
 How does a head-up display work in a high-performance car?Hoe werkt een head-up display in een high-performance auto en welke informatie toont het? Discover the tech, safety alerts, and performance data that sharpen every drive.Author:Time:Oct 18, 2026
 Which trends will shape zonal EV architectures in the next decade?Future trends in zonal EV architectures: explore smarter power distribution, 48V systems, thermal integration, software, and resilient networks shaping next-gen vehicles.Author:Time:Oct 17, 2026
 When does a zonal EV architecture outperform a centralized design?Explore the trade-offs between zonal and centralized EV architectures to identify the best path for harness efficiency, software scalability, safety, and faster EV launches.Author:Time:Oct 16, 2026
 How to compare vendors for zonal EV power architecturesComparing vendors for zonal EV power architectures: assess electrical capability, interface ownership, lifecycle support, and integration risk for smarter sourcing.Author:Time:Oct 15, 2026
 How zonal architectures can improve EV reliability at the system levelHow zonal architectures affect EV reliability: explore fault containment, diagnostics, power resilience, and software strategies for more dependable electric vehicles.Author:Time:Oct 14, 2026